 EN
 English
 中文简体
 Español

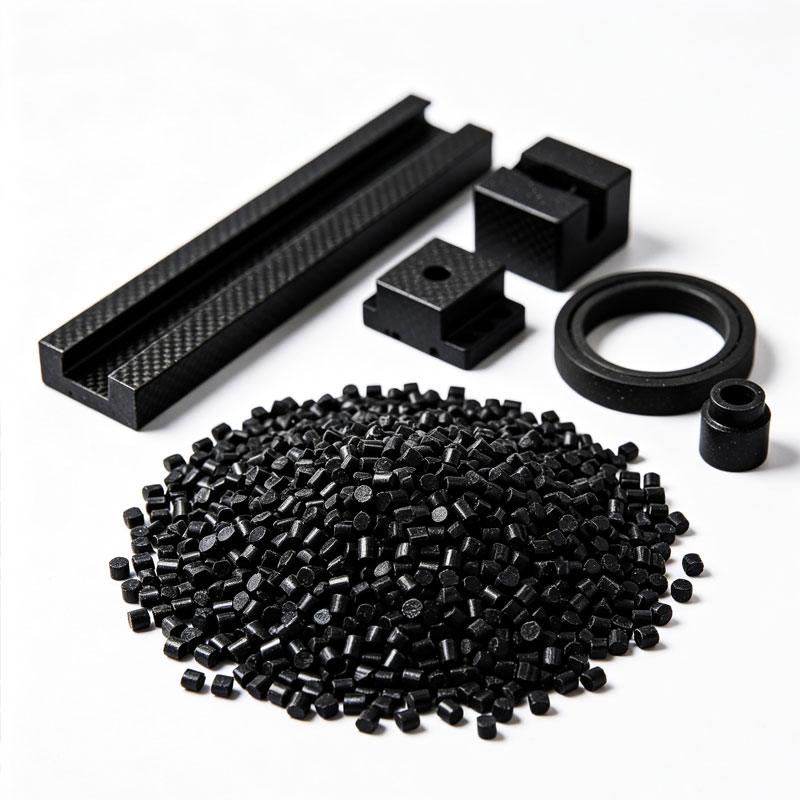
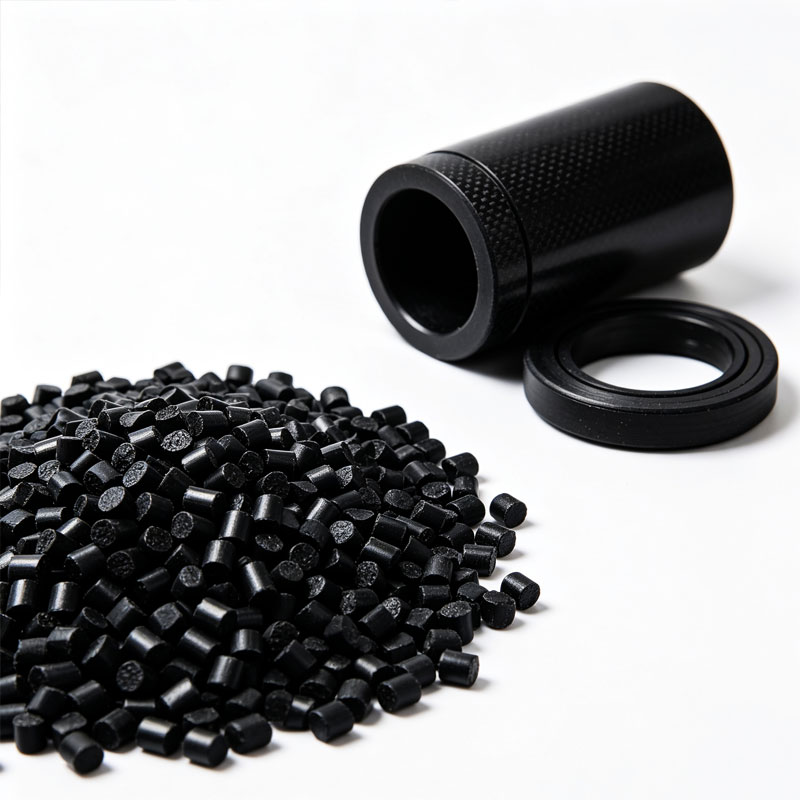
| Product Description | |||||||
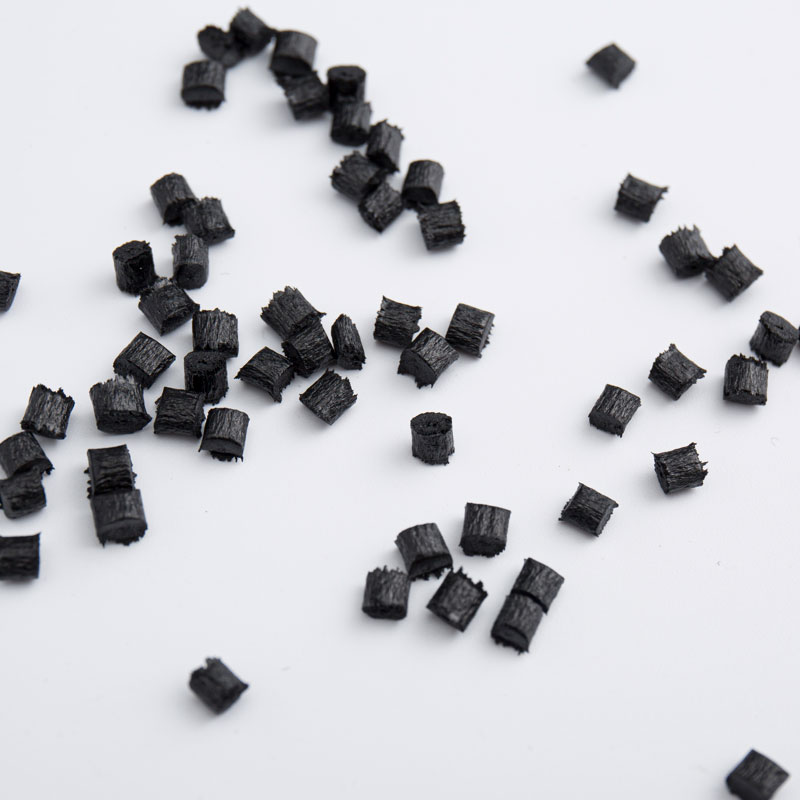
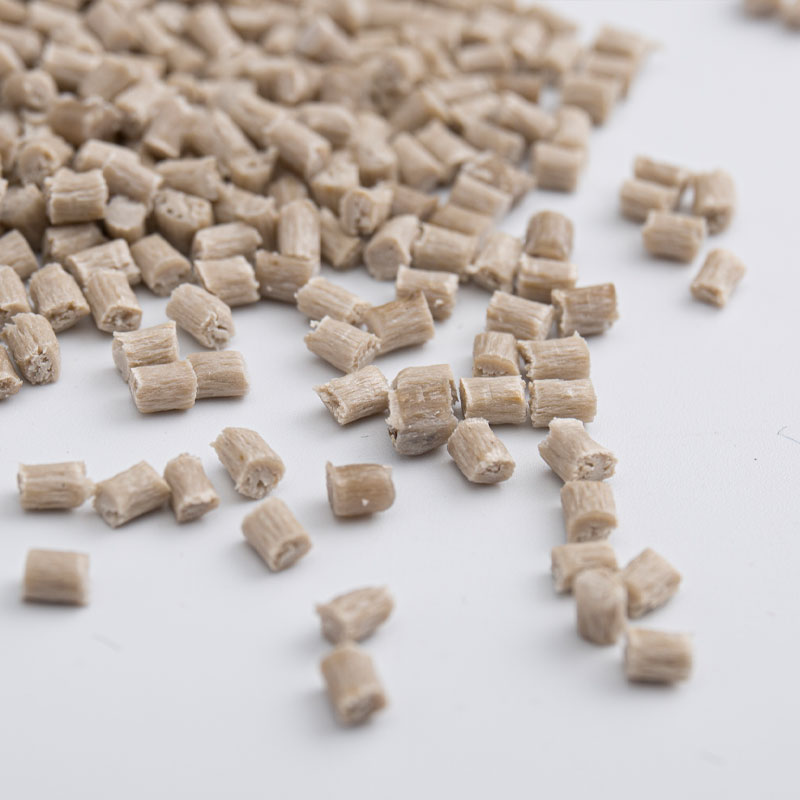
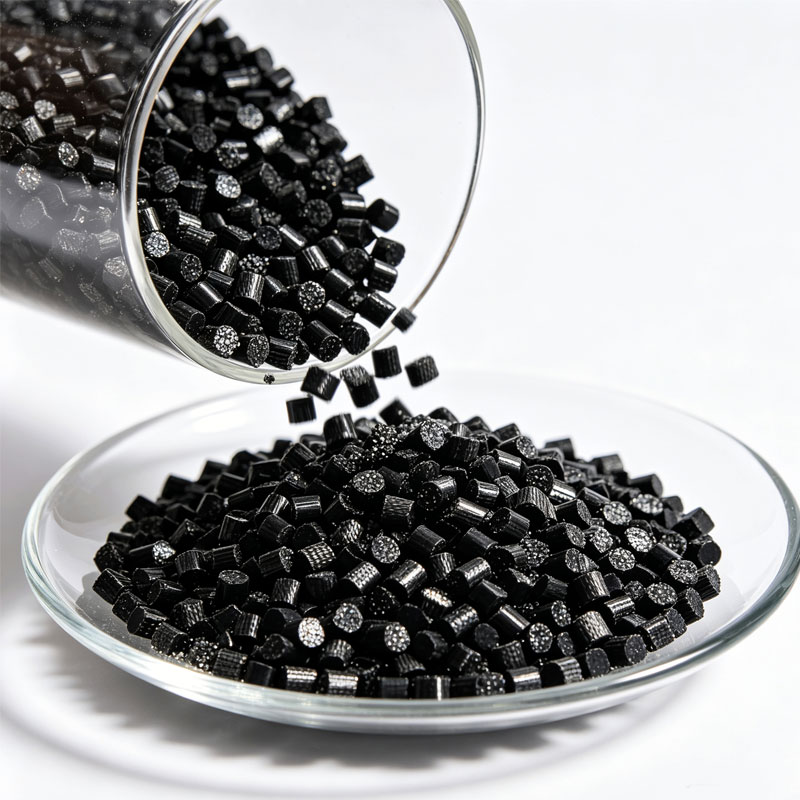
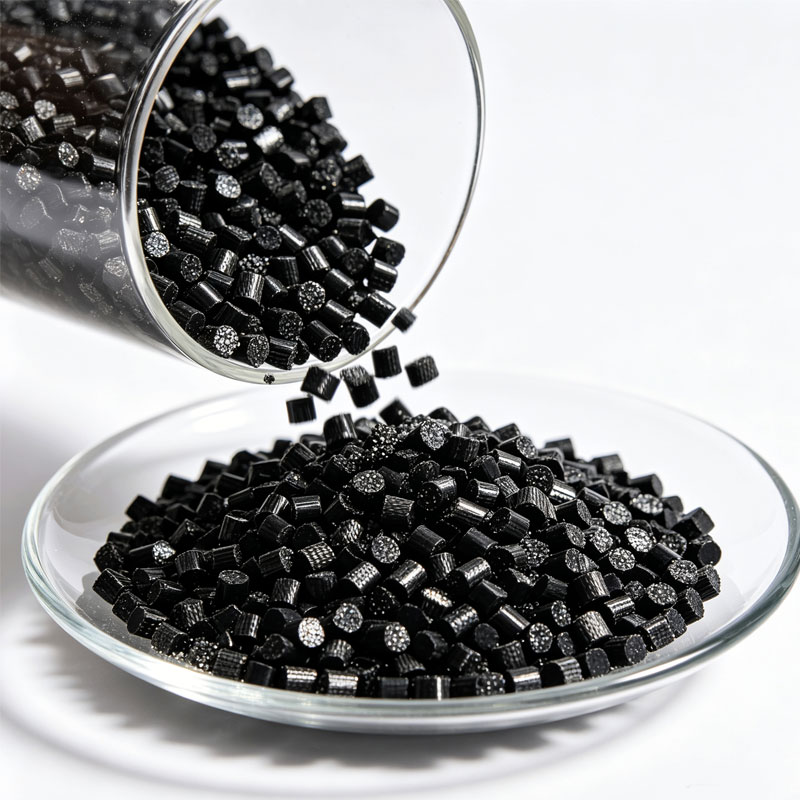
| Resin Identification | Containing carbonfiber,graphite and PTFE conductive grade,high rigidity, good chemical resistance,wear-resistant | ||||||
| Color | Black colour | ||||||
| Main applications | Applications in the robotics field, bearing sleeves, bearing flanges, bullet casings, holsters, scopes | ||||||
| Processing Method | Injection Molding | ||||||
| Typical Properties | Test Method | Test Condition | Value | Unit | |||
| Physical Properties | |||||||
| Density | ISO 1183 | 23℃ | 1.47 | g/cm³ | |||
| Water absorption | ISO 62 | 23℃ Saturation | 0.4 | % | |||
| Shrinkage | ISO 294-4 | Transverse direction | 0.45 | % | |||
| Shrinkage | ISO 294-4 | Flow direction | 0.15 | % | |||
| Mechanical Properties | |||||||
| Tensile Strength | ISO 527 | 50mm/min | 160 | MPa | |||
| Tensile modulus | 12000 | MPa | |||||
| Elongation at Break | 2 | % | |||||
| Flexural Strength | ISO 178 | 2mm/min | 230 | MPa | |||
| Flexural Modulus | 11000 | MPa | |||||
| Izod Unnotched Impact Strength | ISO 180 | 4mm,22℃ | 40 | kJ/M² | |||
| Izod Notched Impact Strength | ISO 180 | 4mm,23℃ | 6 | kJ/M² | |||
| Coefficient of friction | ASTM G99 | dry friction | 0.125 | ||||
| Volume wear rate test | ASTM G133 | 2.0×10⁻⁶ | mm³/(N ·m) | ||||
| Wear scar width test | ASTM G133 | (100N×1000 RPM) | 0.65 | mm | |||
| Thermal Performance | |||||||
| Heat Deformation Temperature | ISO 75 | 1.8MPa | 315 | ℃ | |||
| Heat Deformation Temperature | ISO 75 | 0.45MPa | 330 | ℃ | |||
| Melting temperature | ISO 11357 | 340 | ℃ | ||||
| Linear expansion coefficient | ISO 11359 | Tg Flow, below Tg | 17 | μm/m/℃ | |||
| Linear expansion coefficient | ISO 11359 | Tg Flow, aboveTg | 12 | μm/m/°℃ | |||
| Thermal Performance | |||||||
| Surface Resistance | IEC 60093 | 23℃ | 1.00E+05 | Q/m² | |||
| Volume Resistance | IEC 60093 | 23℃ | 1.00E+07 | Ω.CM | |||
| Dissipation factor | IEC 62631-2-1 | 23℃1MHz | 0.02 | ||||
| CTI | IEC 60112 | 150 | V | ||||
| Flame retardant properties | |||||||
| Flame retardant properties | UL94 | 0.3mm | V0 | Class | |||
| Flame retardant properties | UL94 | 0.5mm | V0 | Class | |||
| Flame retardant properties | UL94 | 1mm |
V0 | Class | |||
| Flame retardant properties | UL94 | 1.5mm | V0 | Class | |||
| (GWFI)Glow wire flammability index | IEC60695-2-12 | 0.75mm | 960 | ℃ | |||
| (GWFI)Glow wire flammability index | IEC60695-2-12 | 1.5mm | 960 | ℃ | |||
| (GWFI)Glow wire flammability index | IEC60695-2-12 | 3mm | 960 | ℃ | |||
| (GWFI)Glow wire flammability index | IEC60695-2-13 | 0.75mm | 850 | ℃ | |||
| (GWFI)Glow wire flammability index | IEC60695-2-13 | 1.5mm | 850 | ℃ | |||
| (GWFI)Glow wire flammability index | IEC60695-2-13 | 3mm | 960 | ℃ | |||
NOTE: (1) The data provided are typical values and are only for reference by customers. They do not guarantee the minimum or maximum values for quality
indicators or any other purposes. (2) Different colors may have different performance characteristics.
Note: The data and information in this document are based on our current understanding and experience.If there are new understandings and experiences in the future, it is possible that the information and data in this document may be modified without prior notice. Due to the varying conditions and applicable laws in different regions and at different times, customers are responsible for determining whether the products and product information in this document are suitable for their use,and ensuring that their work sites and methods of handling products comply with applicable laws and other government regulations. Lishumaterial has no responsibility or obligation for the information and data in this document, and has not provided any guarantees. All implied warranties regarding the marketability of the products or the applicability for a specific purpose are expressly excluded in this document. For more details, please visit the company website: www.lisumaterial.com.
| Plastic Drying | |
| Drying Time | 2~4HRS |
| Drying Temperature | 130~150℃ |
| Drying Equipment | Hot air dryer |
| Drying Type | Continuous drying (production process) |
| Injection Molding Process | |
| Nozzle Section | 370~-390°C |
| Plastics Section | 380~-400°C |
| Conveying Section | 360~380°C |
| Maximum Injection Temperature | 450°C |
| Injection Pressure | 30-70MPa |
| Injection Speed | 30~75mm/s |
| PlastizatirVlit | 35~70MPa,50-100mm/s |
| Plasticization Back Pressure | 20-60MPa |
| Recommended Mold Temperature | 170~210°C |
NOTE: The above injection molding process should vary according to different conditions such as the shape of the product, the design of the mold, and the specifications of the injection machine. Specific adjustments should be made based on the actual situation.